Define the rivet family
Supply head, shank and length dimensions with representative parts. Keep visually similar lengths or head styles separately identified so a trial does not assume they are interchangeable.
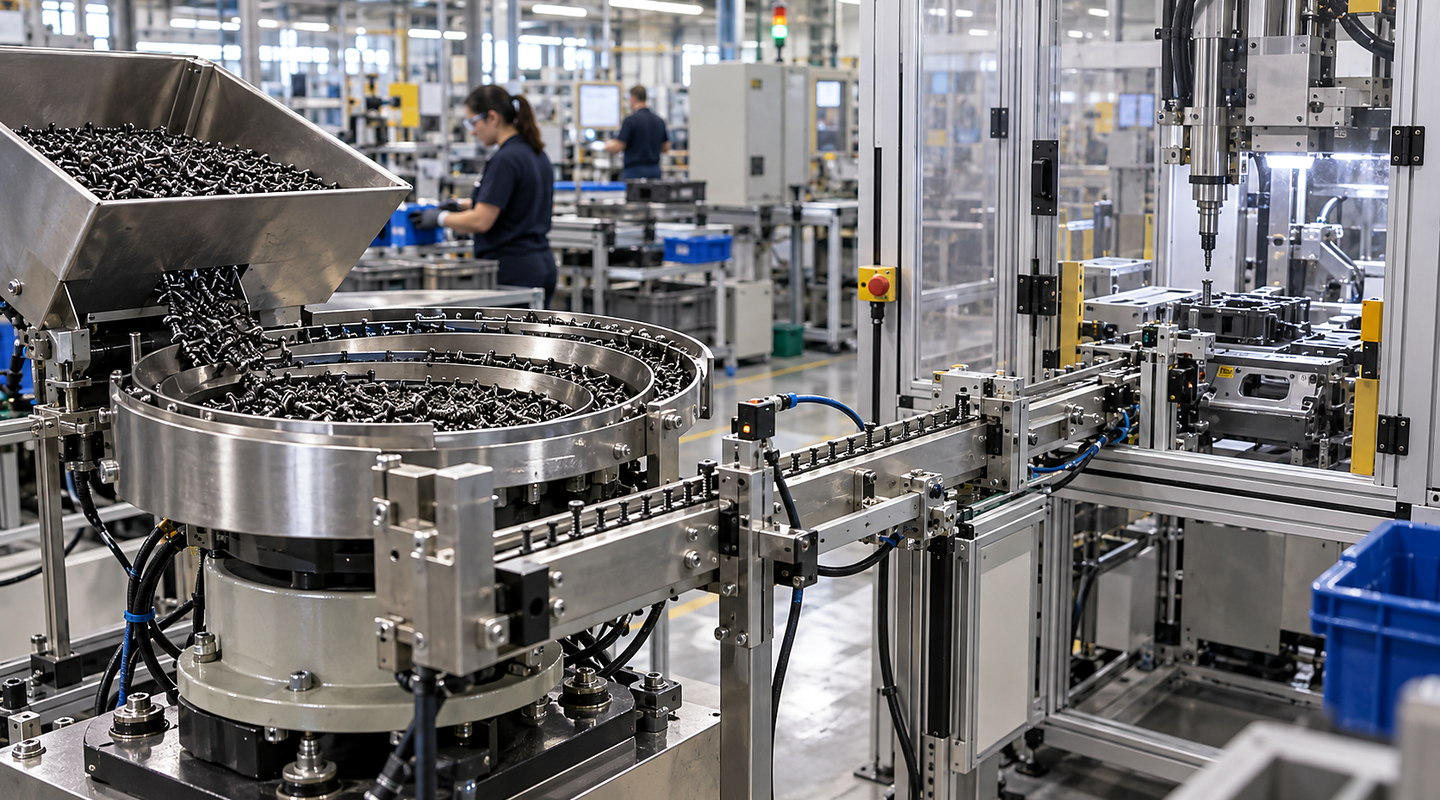
Plan rivet feeding systems around real component variation, bulk condition, orientation, usable delivery rate and the downstream interface. Discuss representative part trials with Sorting Solutions.
Speak directly with Sorting Solutions about rivet orientation and presentation.
Supply rivets across the head, shank and length range, including the normal bulk condition. Define the orientation and transfer position needed by the riveting tool. Trial single-part release and delivery, with checks for mixed variants, bent rivets and the recovery sequence when the receiving tool cannot accept a part.
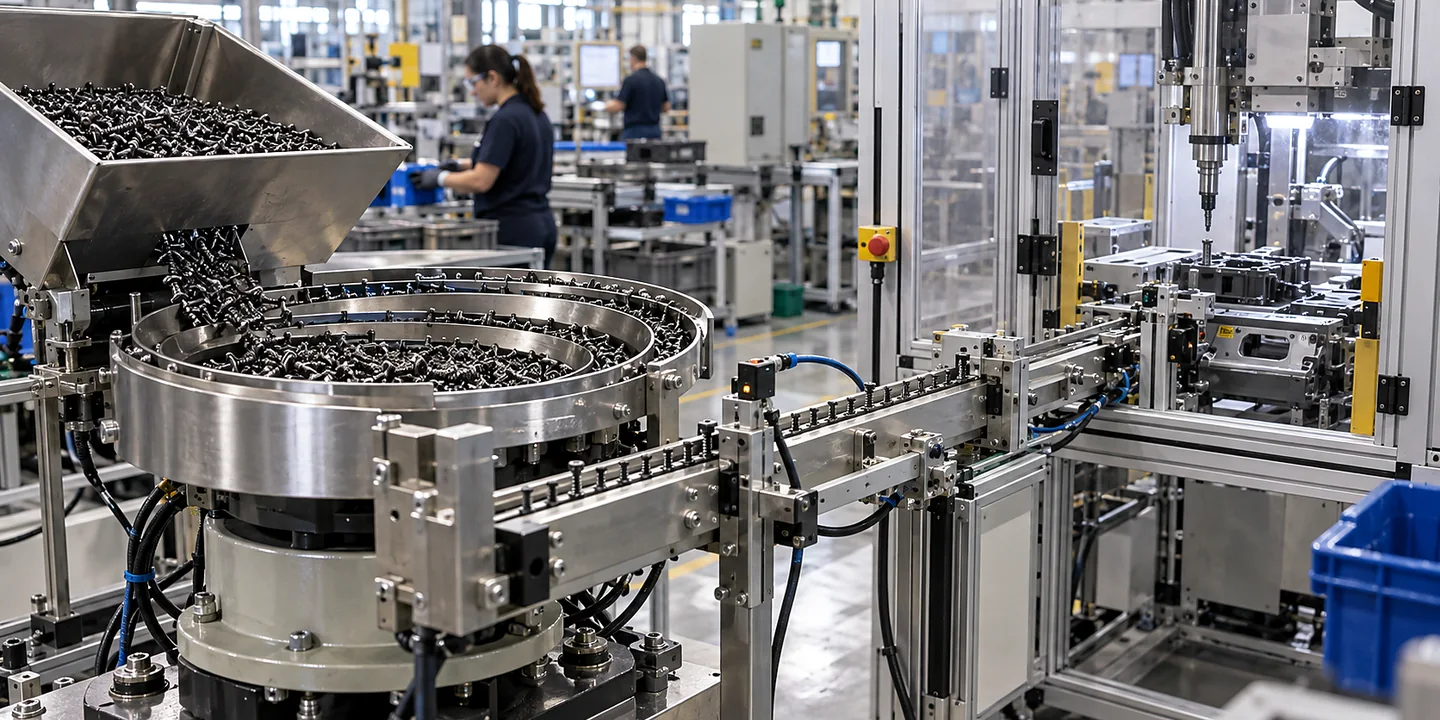
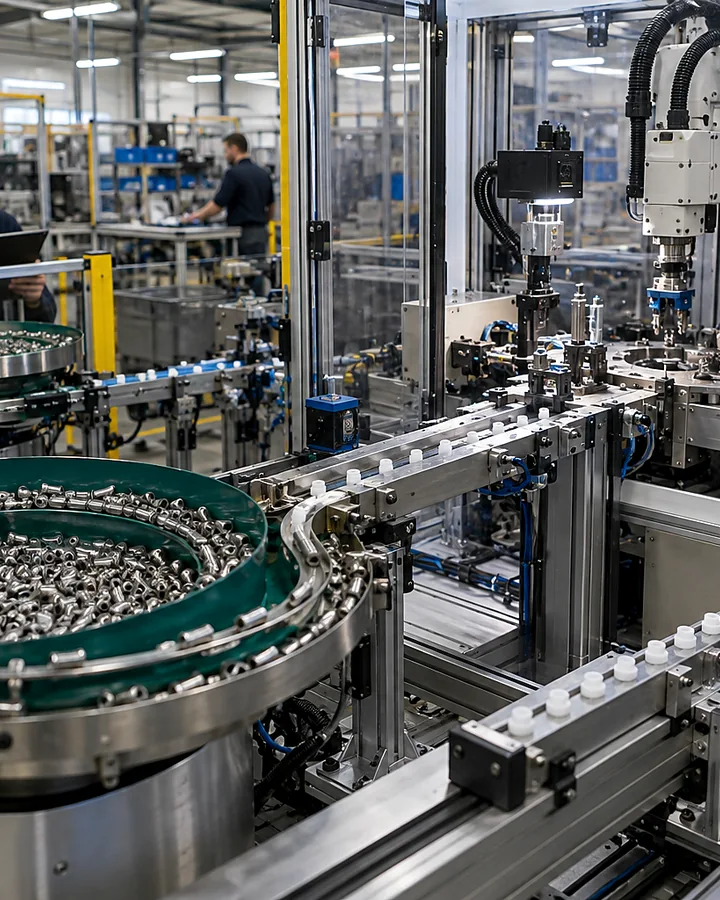

The rivet feeder and riveting operation share one interface: a correctly identified rivet must arrive in the right orientation and be accepted by the tool.
Supply head, shank and length dimensions with representative parts. Keep visually similar lengths or head styles separately identified so a trial does not assume they are interchangeable.
Include the finish and surface condition used in production. Show whether rivets arrive mixed, tangled or with damaged examples that must be excluded before delivery.
Provide the tool’s receiving position and the feature used to locate the rivet. Head-up, head-down or another presentation must follow the assembly requirement, not just the easiest feeder discharge.
Record the route between release and tool, including available space and any changes of direction. Prove delivery using the intended installation rather than only the feeder outlet.
Define the tool-ready, part-present and transfer-complete conditions. Include a receiving tool that does not accept a rivet so the next release does not create an uncontrolled double feed.
Agree how a blockage is cleared and how remaining parts are removed before a variant change. Track the feeder tooling and settings required for each approved rivet.
The right choice changes with component geometry and variation for rivet orientation & presentation, surface, fragility and entanglement behaviour, your line layout and required results.
Measure rivets accepted at the required assembly presentation. Record missed deliveries, duplicates, incorrect orientation and operator interventions separately from circulation inside the feeder.
Inspect the head and shank for damage relevant to the fastening process. Include normal replenishment and restart conditions, when the delivery pattern may differ from steady running.
Send rivet samples, drawings, required rate, tool details and a layout or video of the present process. Identify the most difficult variant and any restriction on contact or surface marking.
Use the rivet feeding systems specification checklist to prepare the application, then agree the acceptance checks and production records before comparing proposals.
Your final solution for rivet orientation and presentation must reflect the law, current standards and site-specific risks that apply to your installation.
The feeder must deliver the specified rivet in the required condition; the assembly process must establish the joint. Separating those responsibilities makes a trial and a fault record more useful.
Provide the actual head, shank and length range and any orientation-critical features. Identify look-alike variants and what makes them incompatible with the receiving tool. A general request for a rivet feeder does not define whether one track and transfer arrangement can handle the proposed range.
State whether the tool collects from a fixed nest or receives a transferred rivet, and what confirms the receiving point is ready. Include support and alignment at that point. Successful travel along the track does not prove that the rivet enters the tool in the condition needed for assembly.
Include an occupied receiver, a missing rivet and a stopped assembly cycle in the agreed safe demonstration. Confirm what prevents a second release into an uncertain route and how the retained part is dealt with. Keep the feeder state and the tool state visible in the recovery instructions.
Document the physical change parts and how the old rivet size is removed from the hopper, track and transfer route. Inspect the first accepted deliveries after changeover. A batch counter resetting to zero does not establish that every previous rivet has been cleared from the machine.
Compare rivet feeding and transfer requirements — explore the existing guidance